
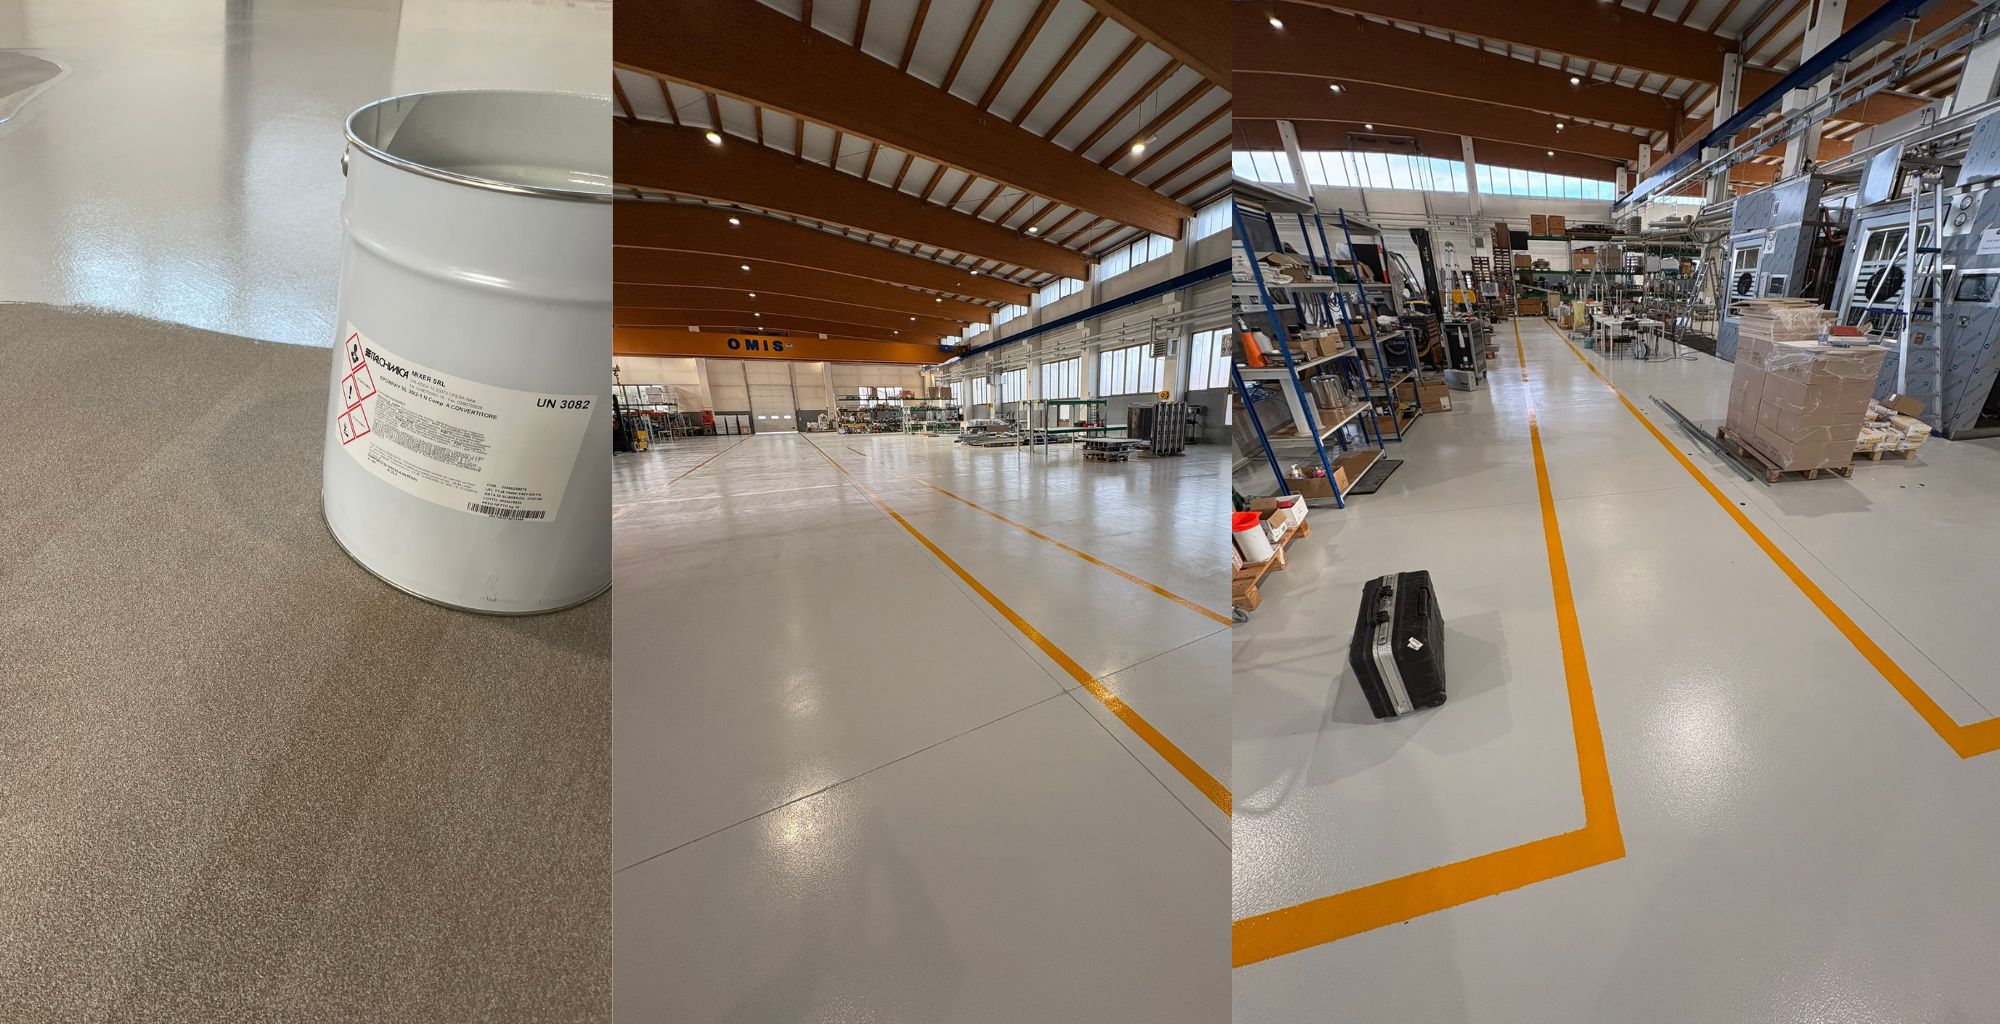
The epoxy multilayer flooring system is one of the most reliable solutions for industrial environments requiring durability, chemical resistance, and long-term performance. This case history showcases a complete application in a large production facility, where performance, aesthetics, and safety were equally critical.
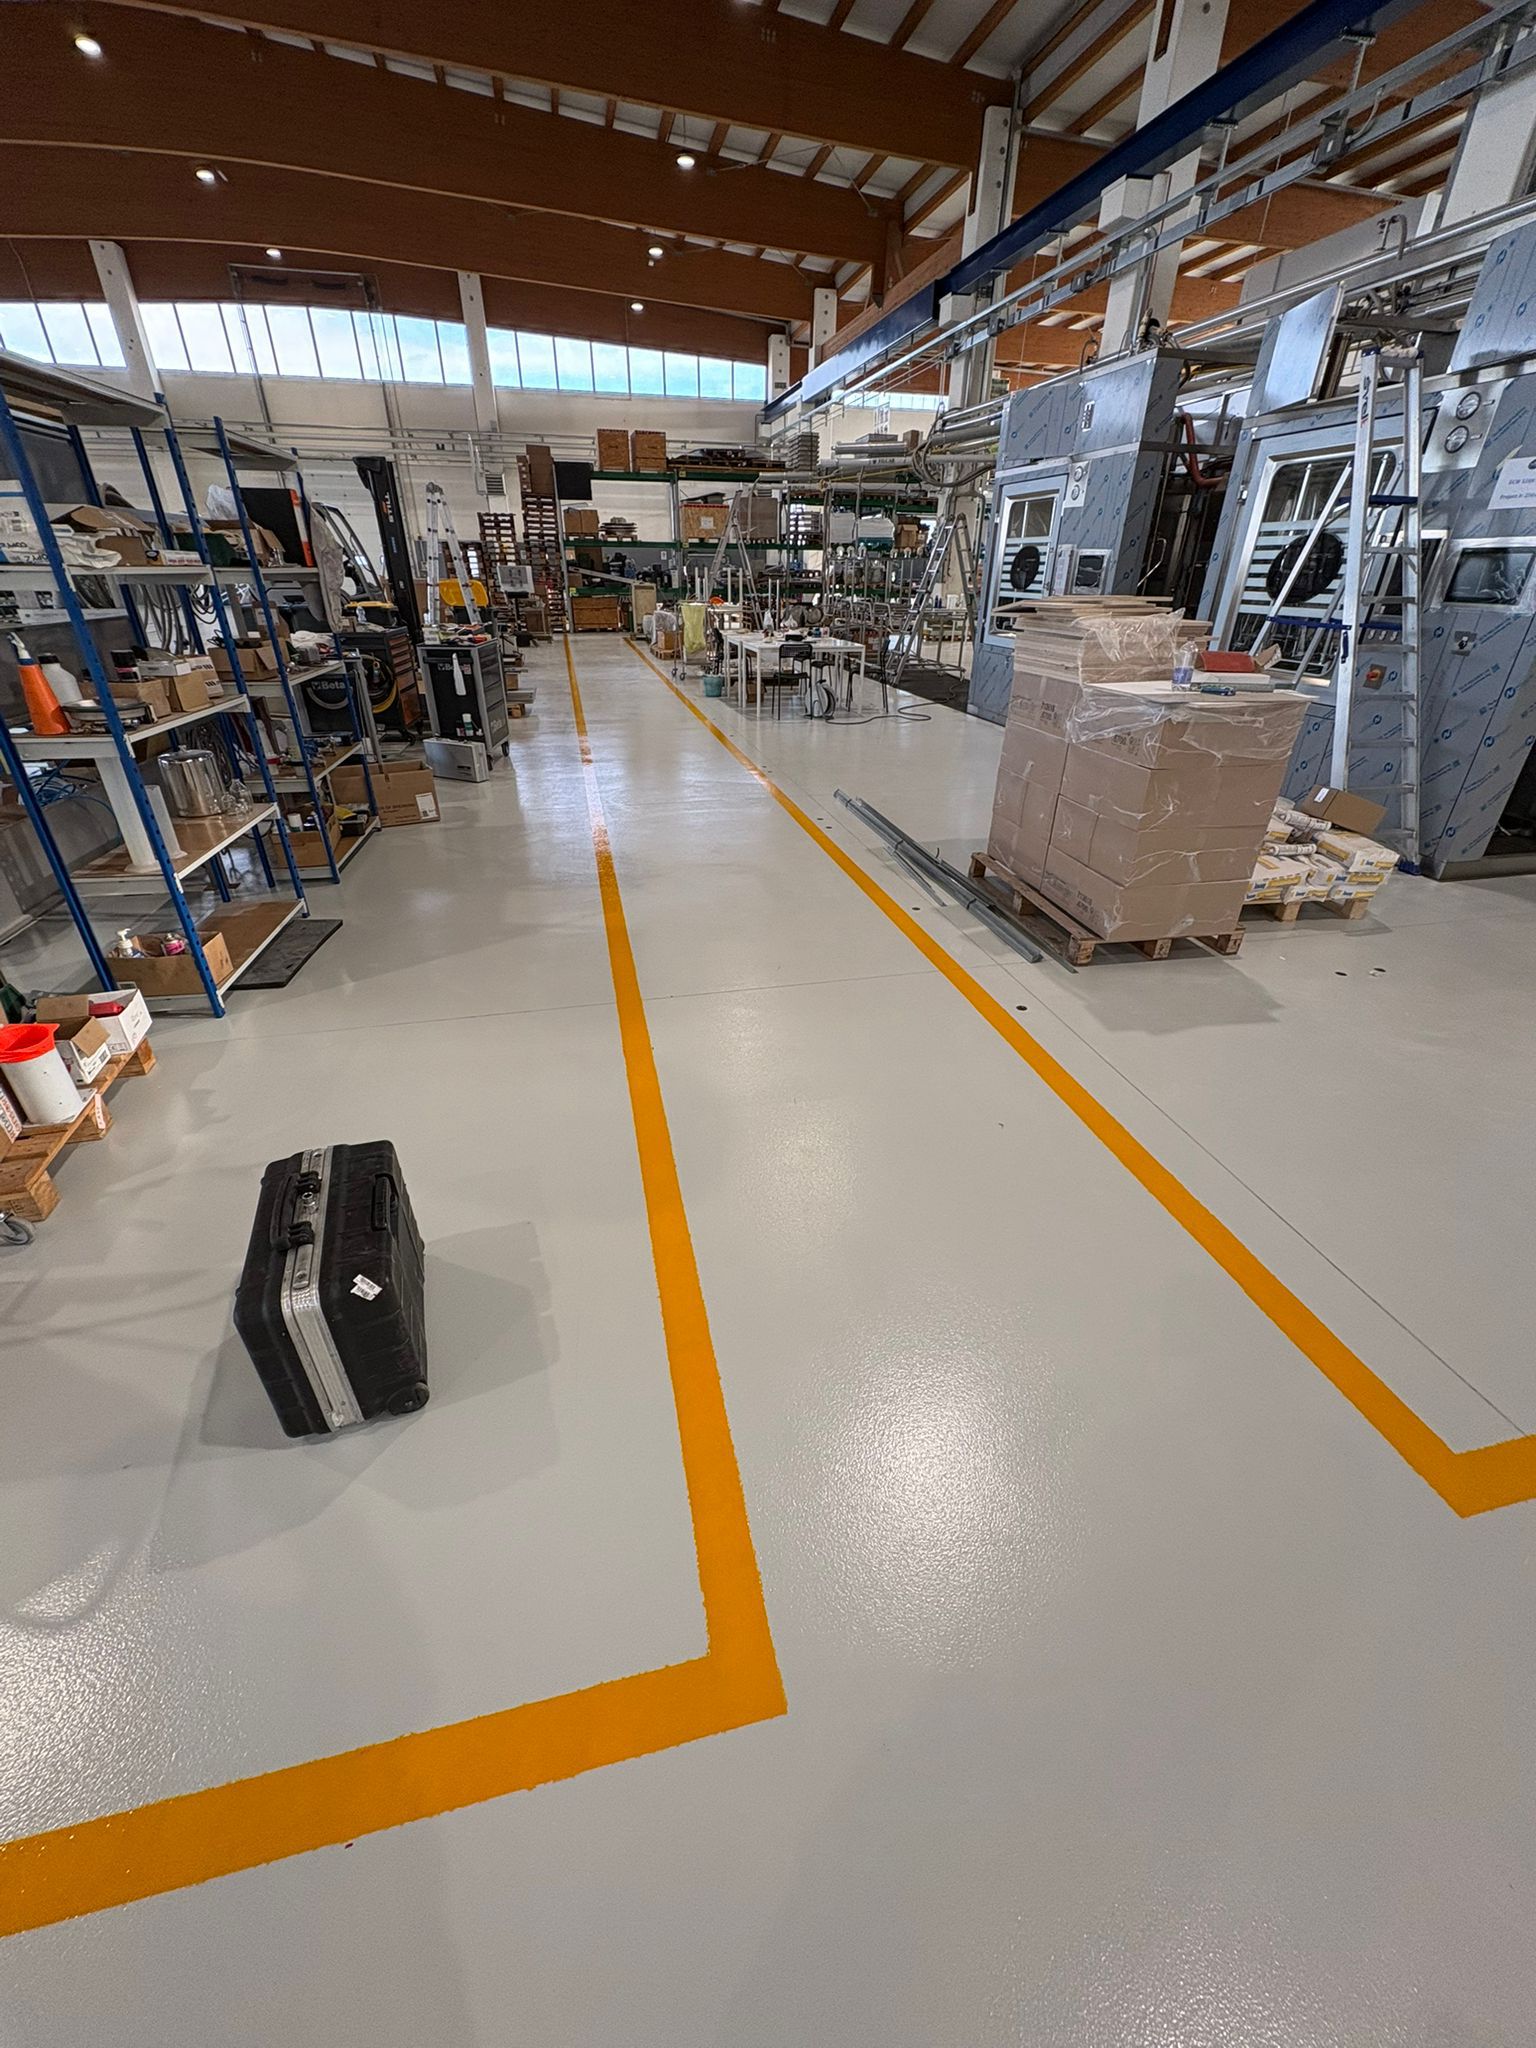
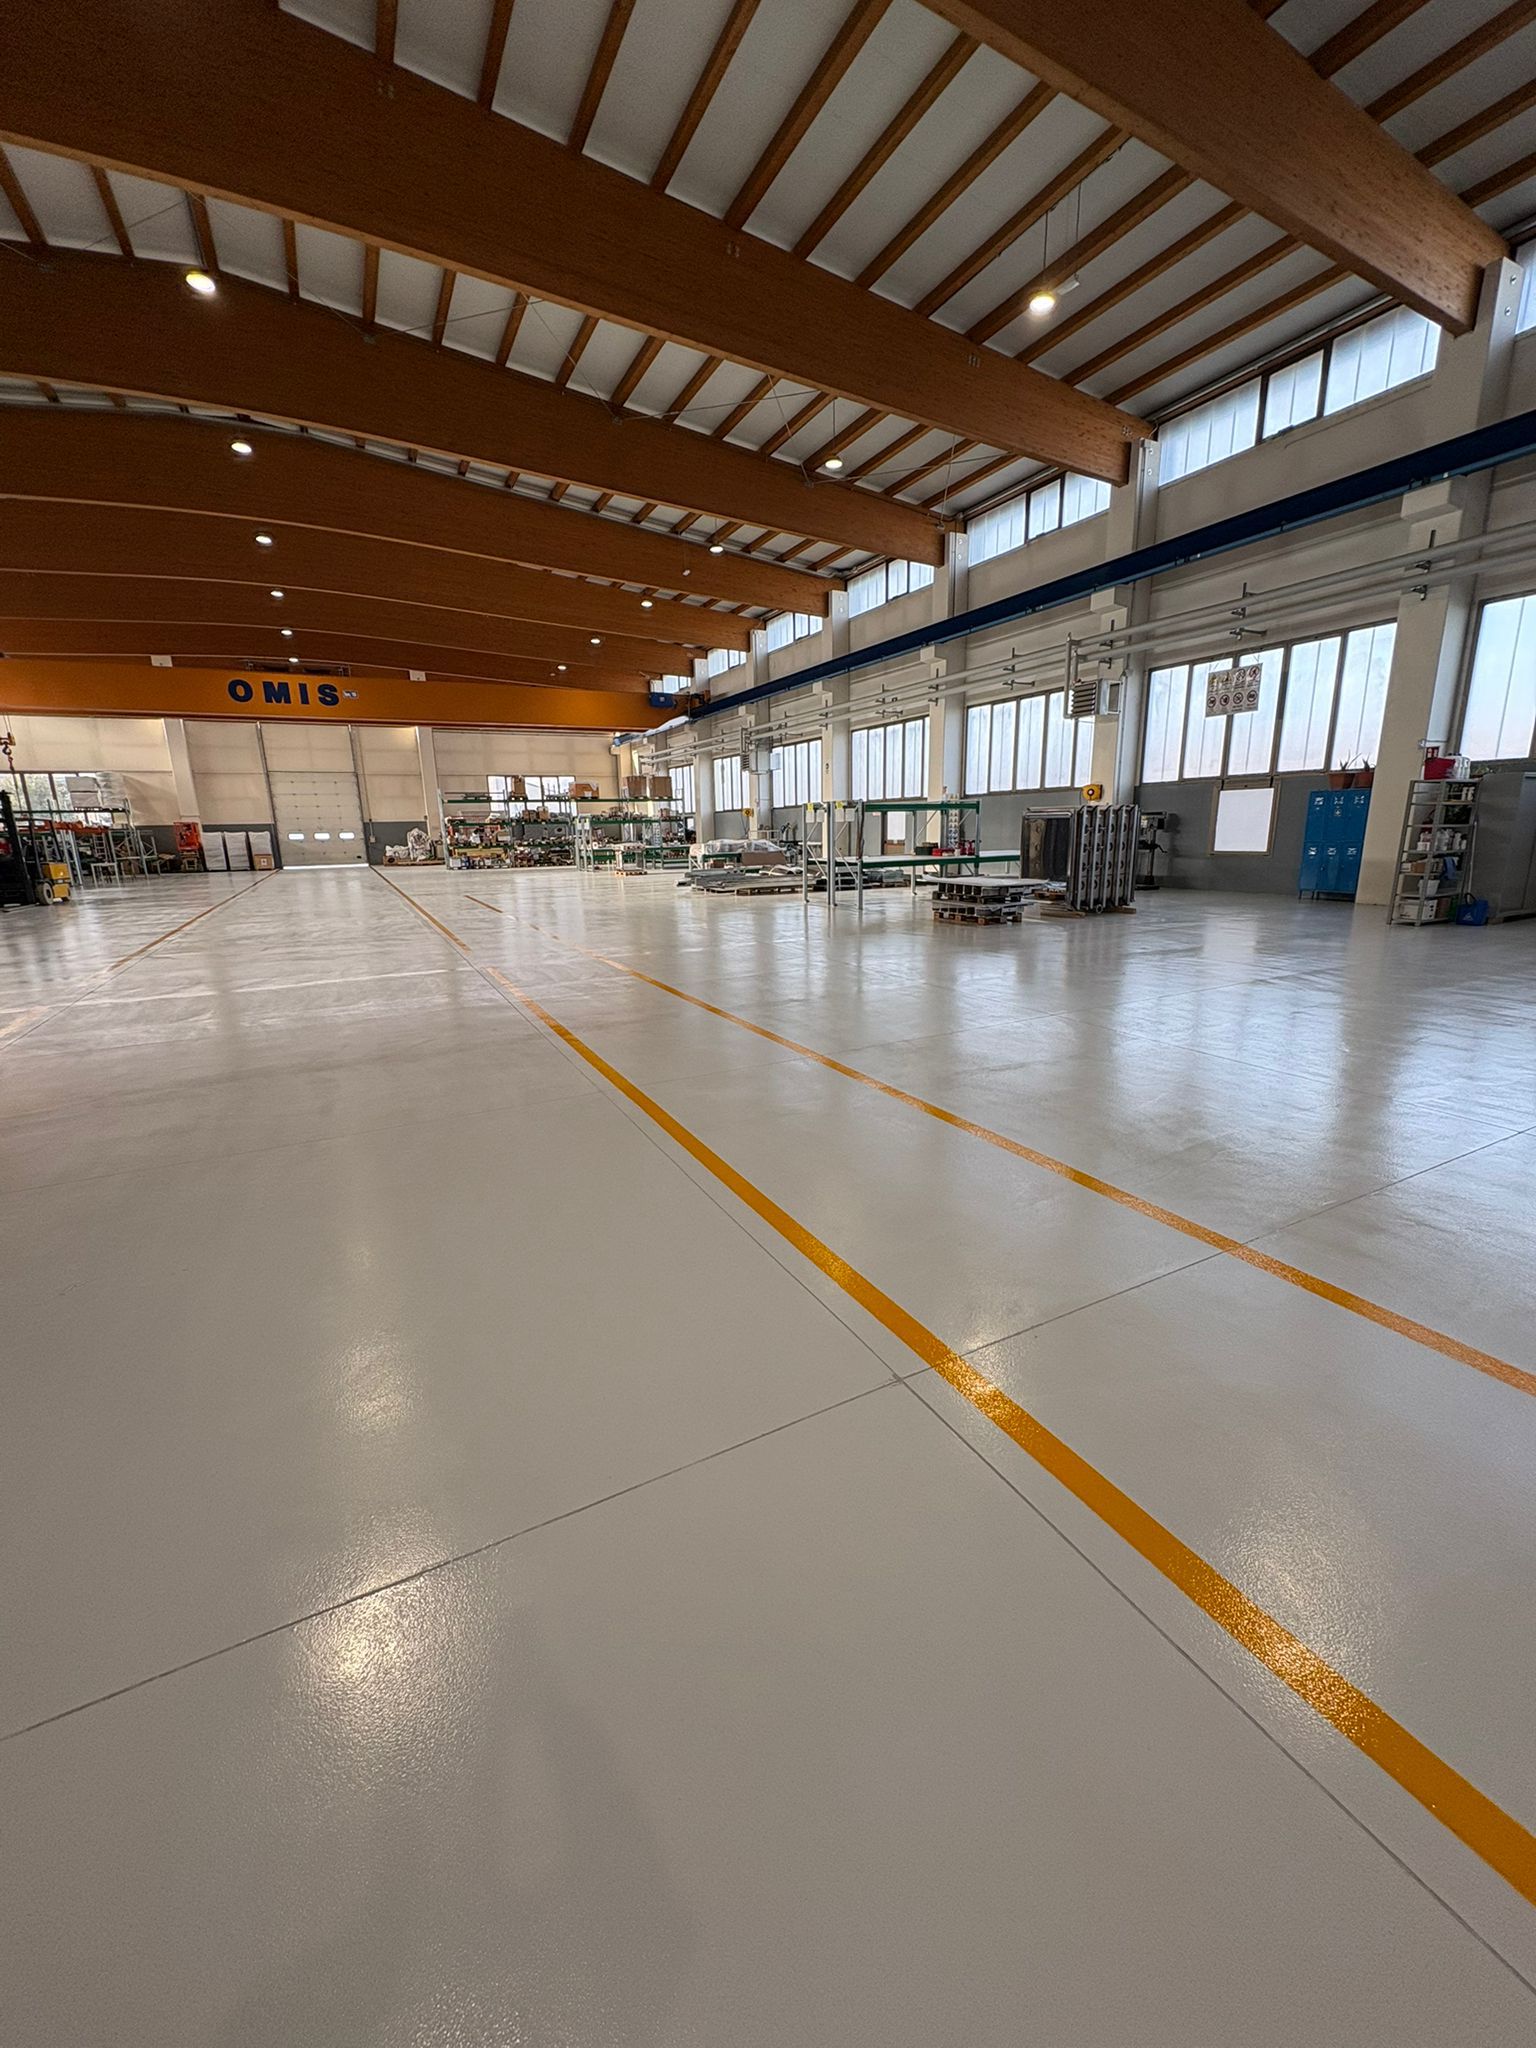
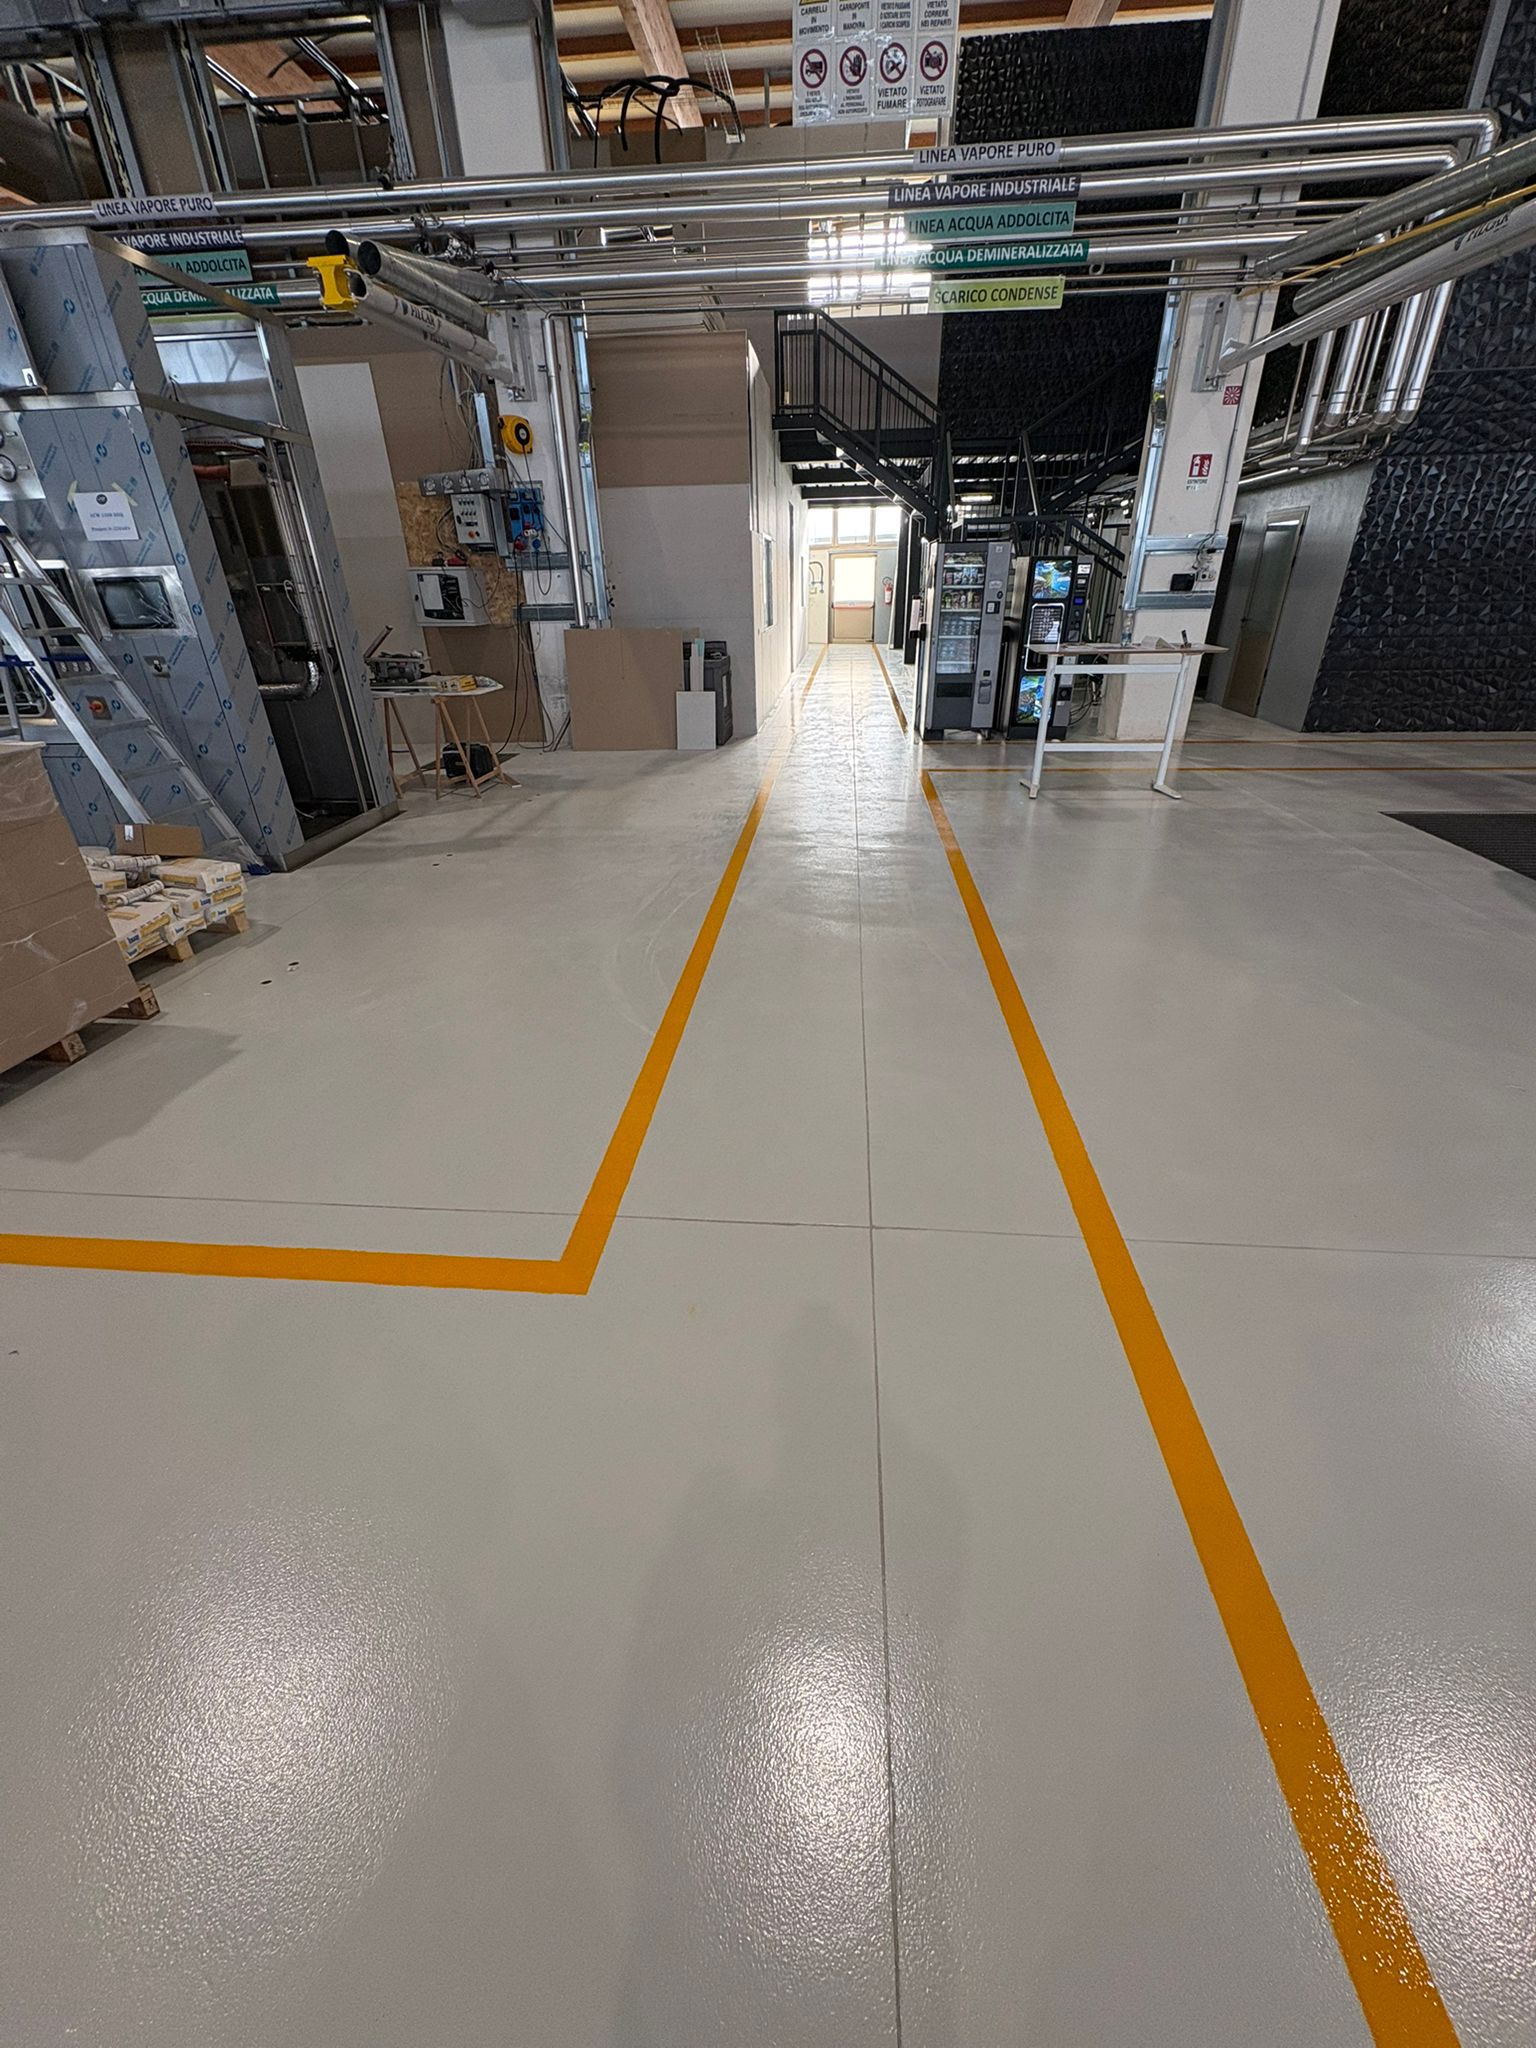
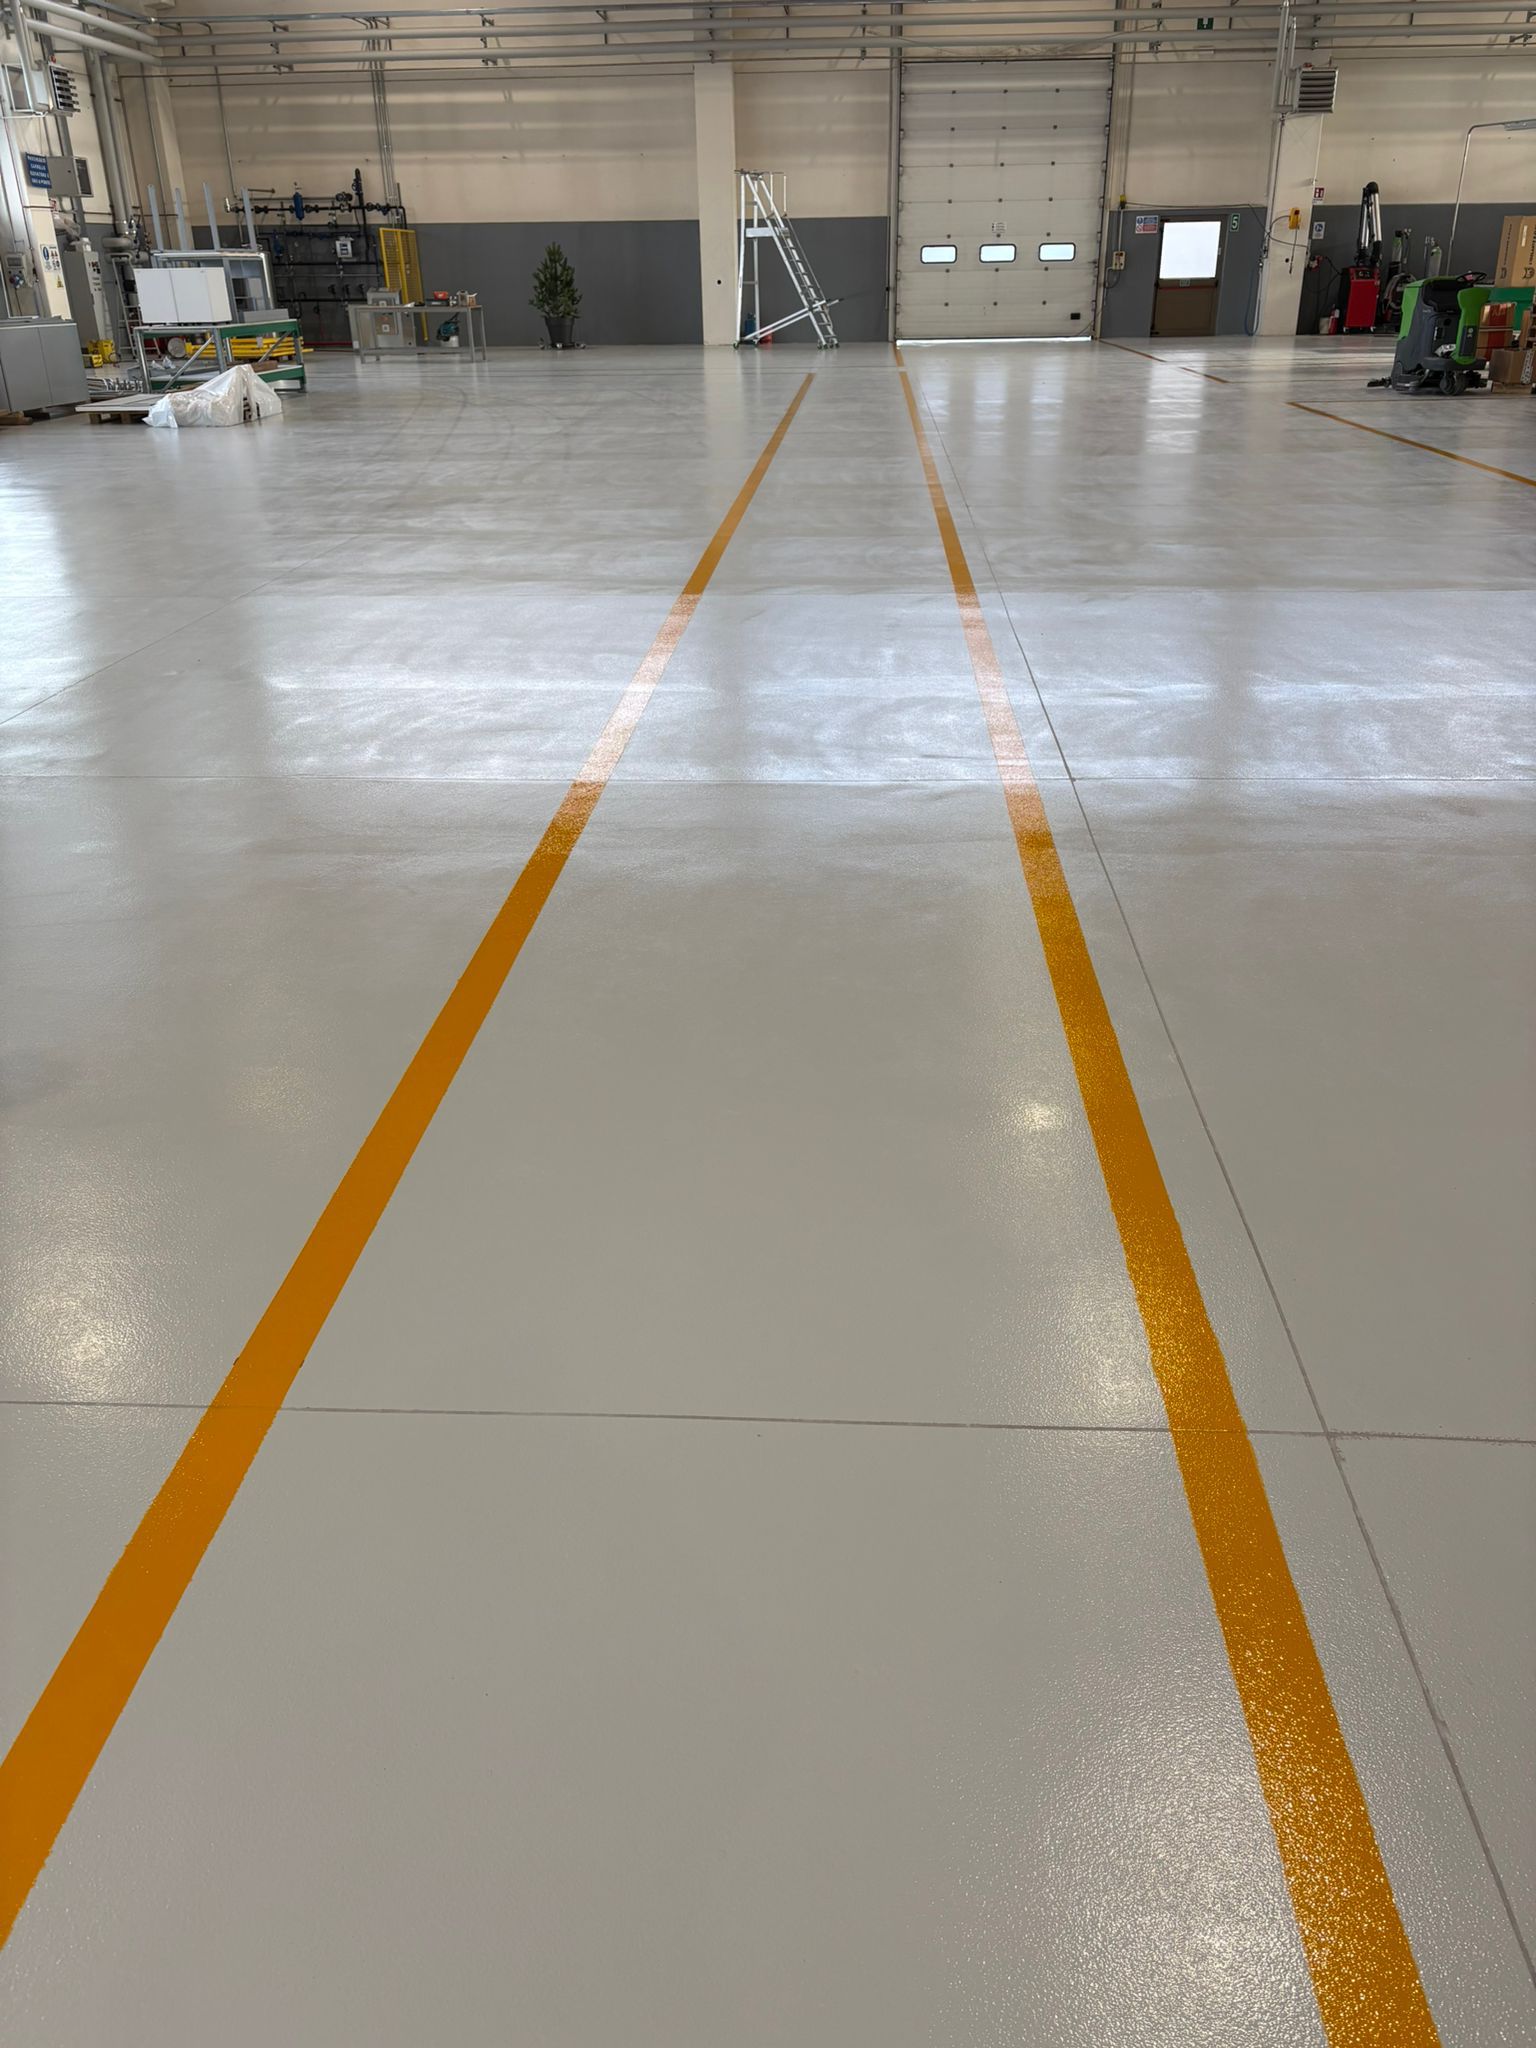
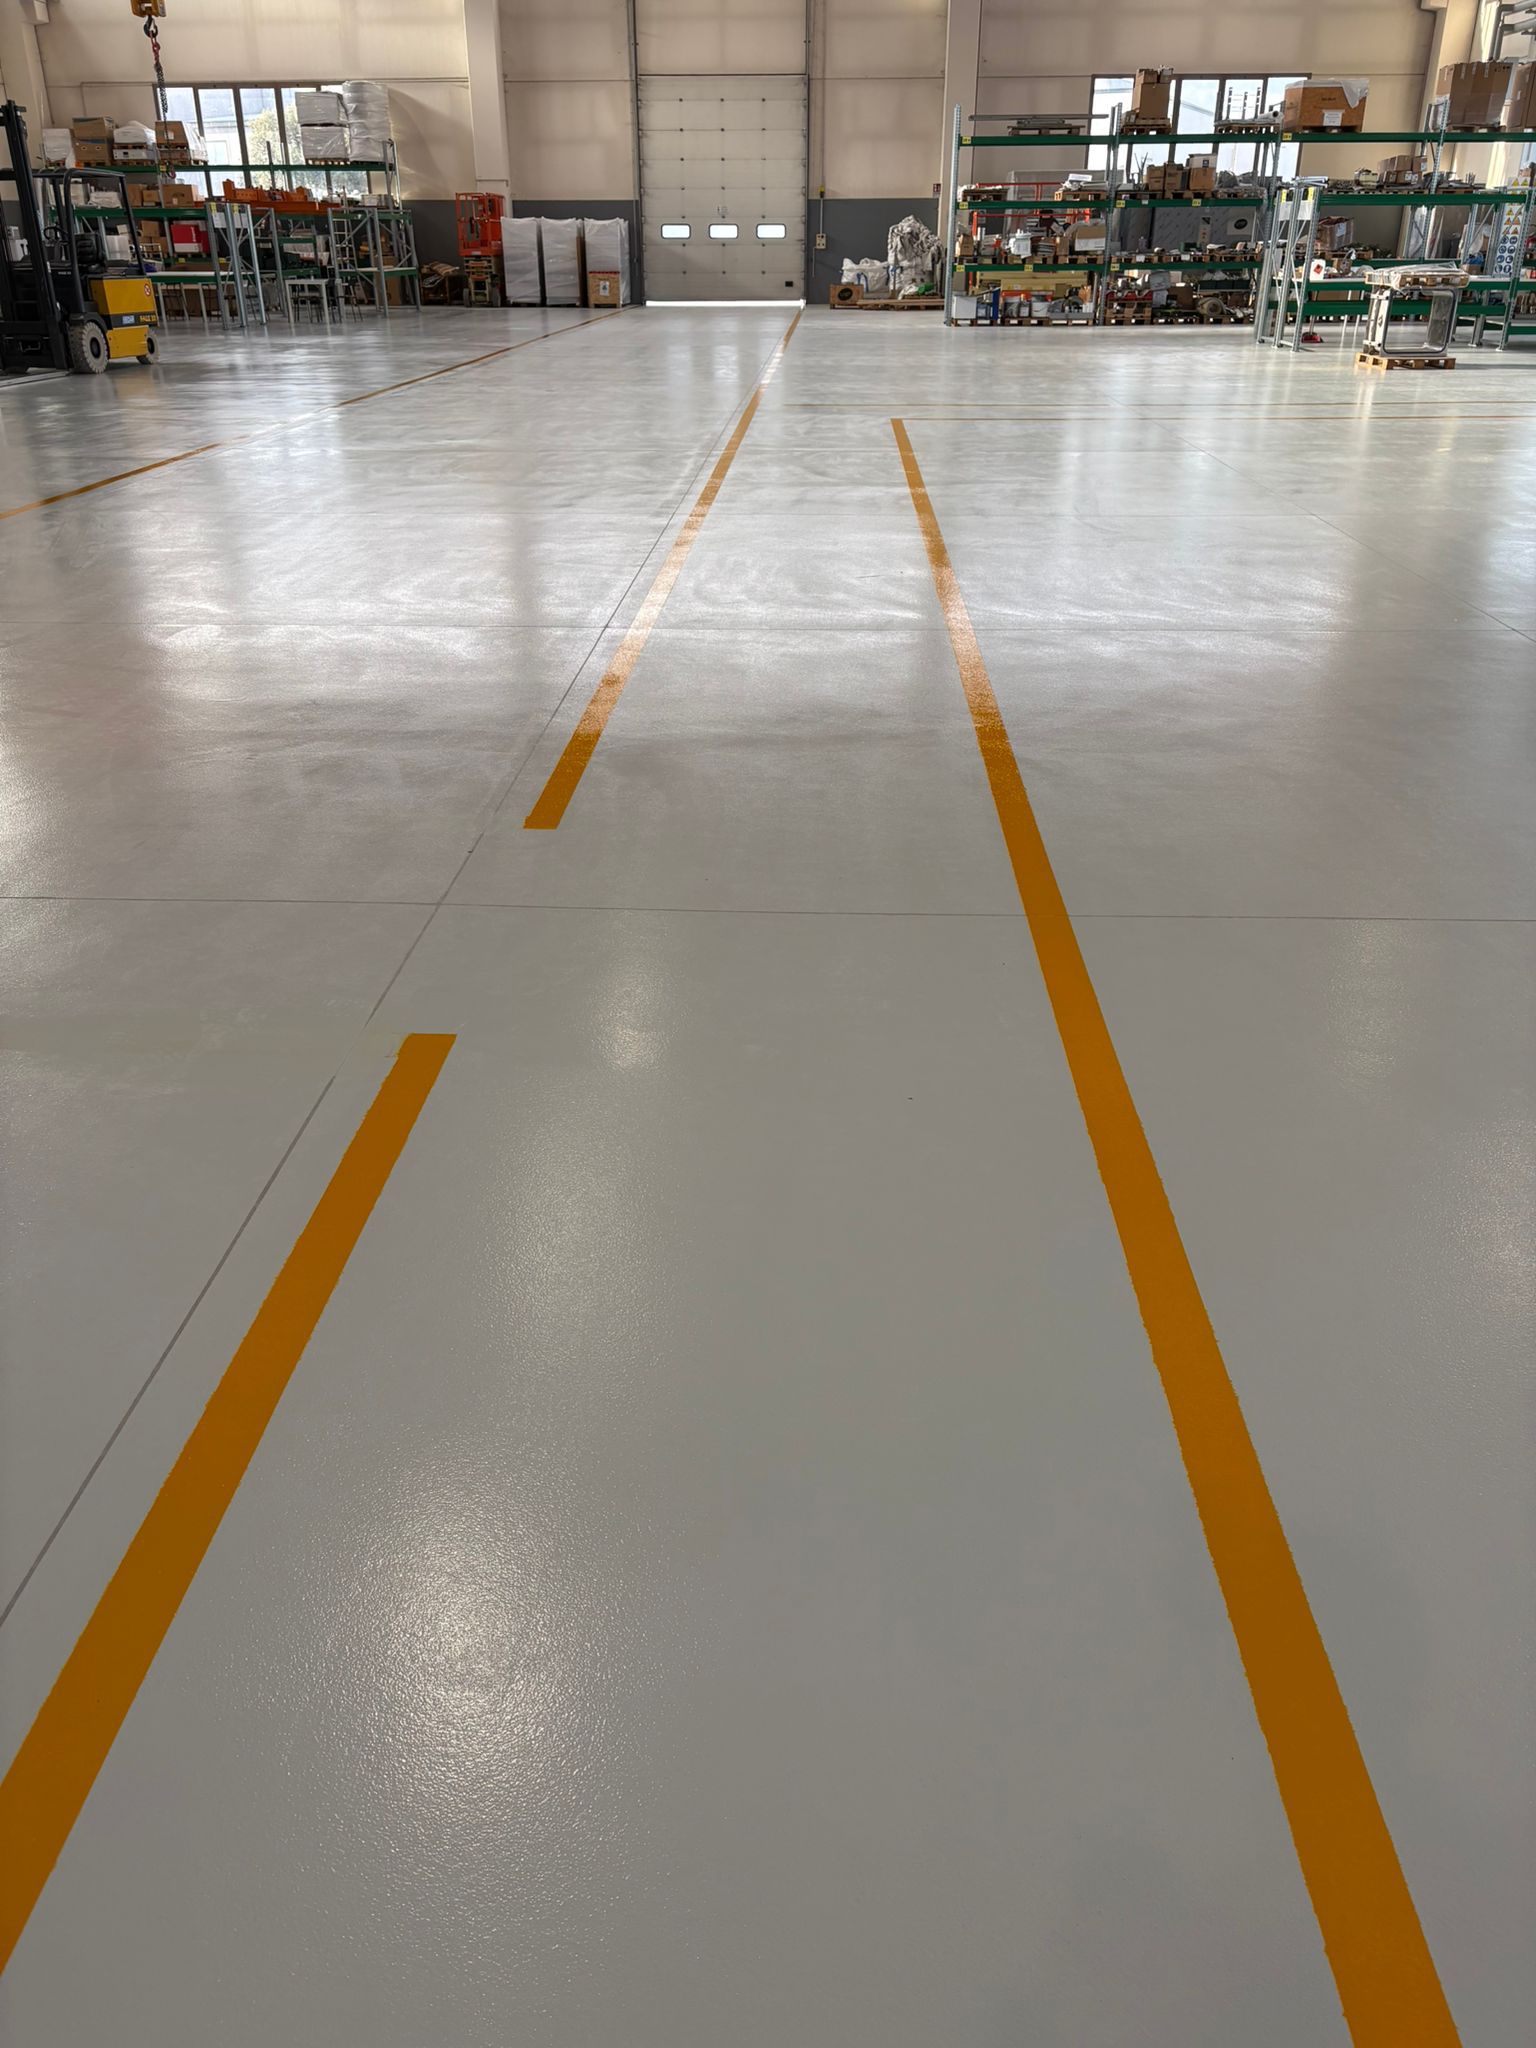
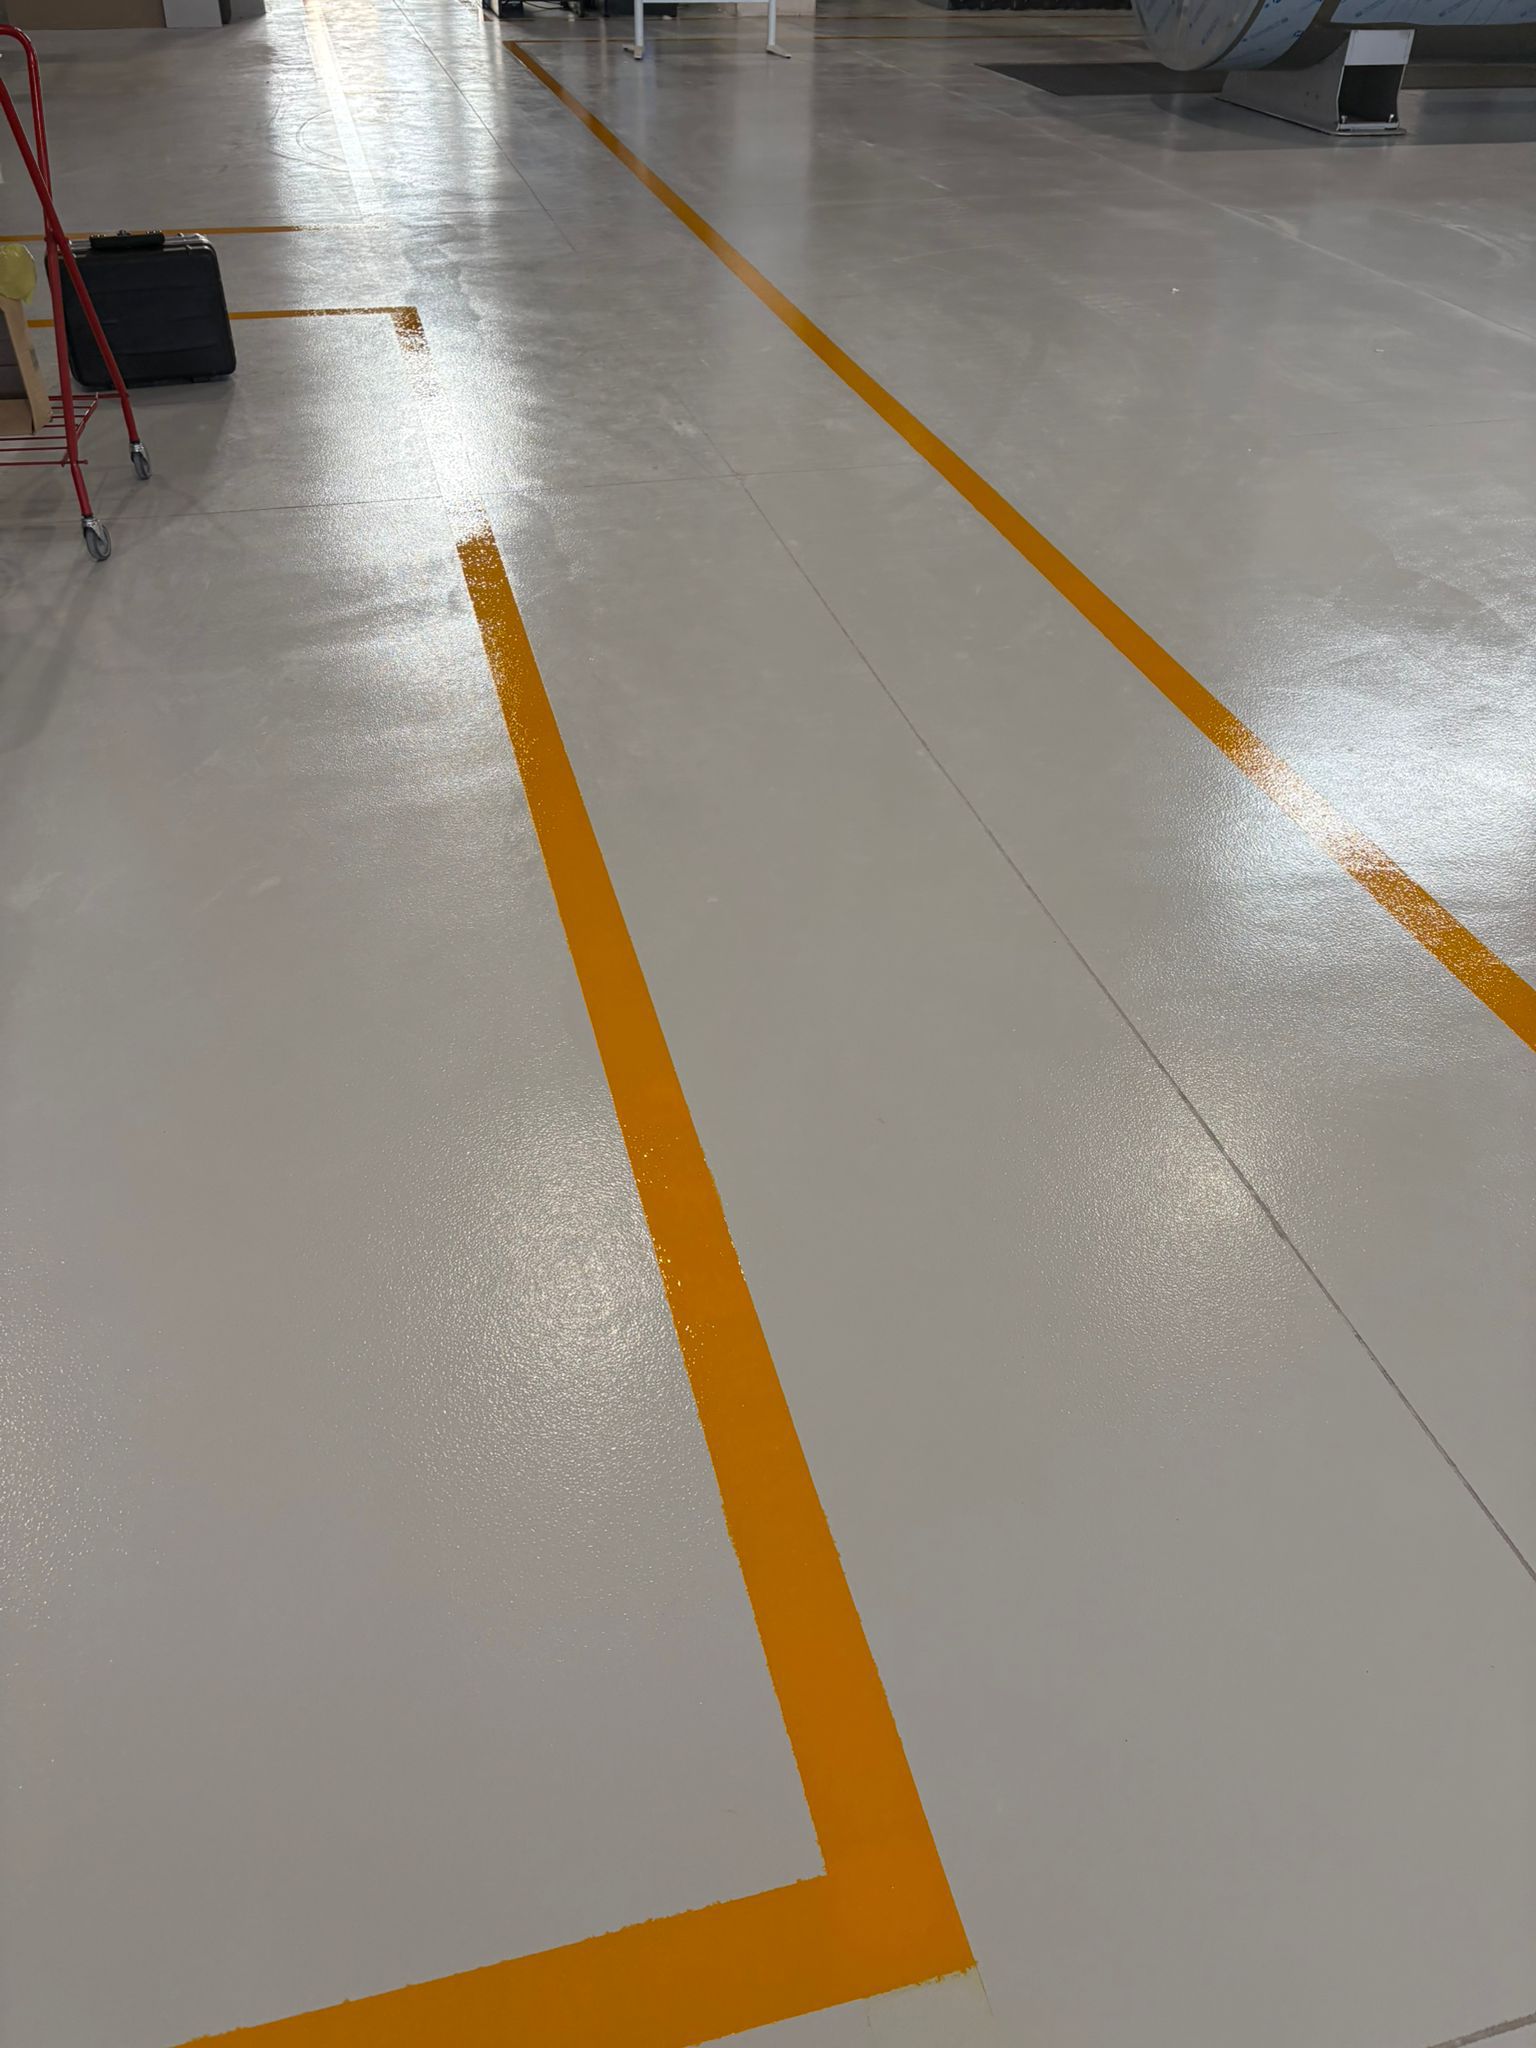
As visible from the job site images, the final result delivers a seamless, uniform surface with high reflectivity, integrated safety markings, and excellent resistance to heavy traffic.
The Challenge
The project involved the renovation of a large industrial warehouse floor, characterised by:
- Heavy forklift traffic
- Exposure to oils, detergents, and chemicals
- Need for clear safety line markings
- Requirement for easy cleaning and dust-free surfaces
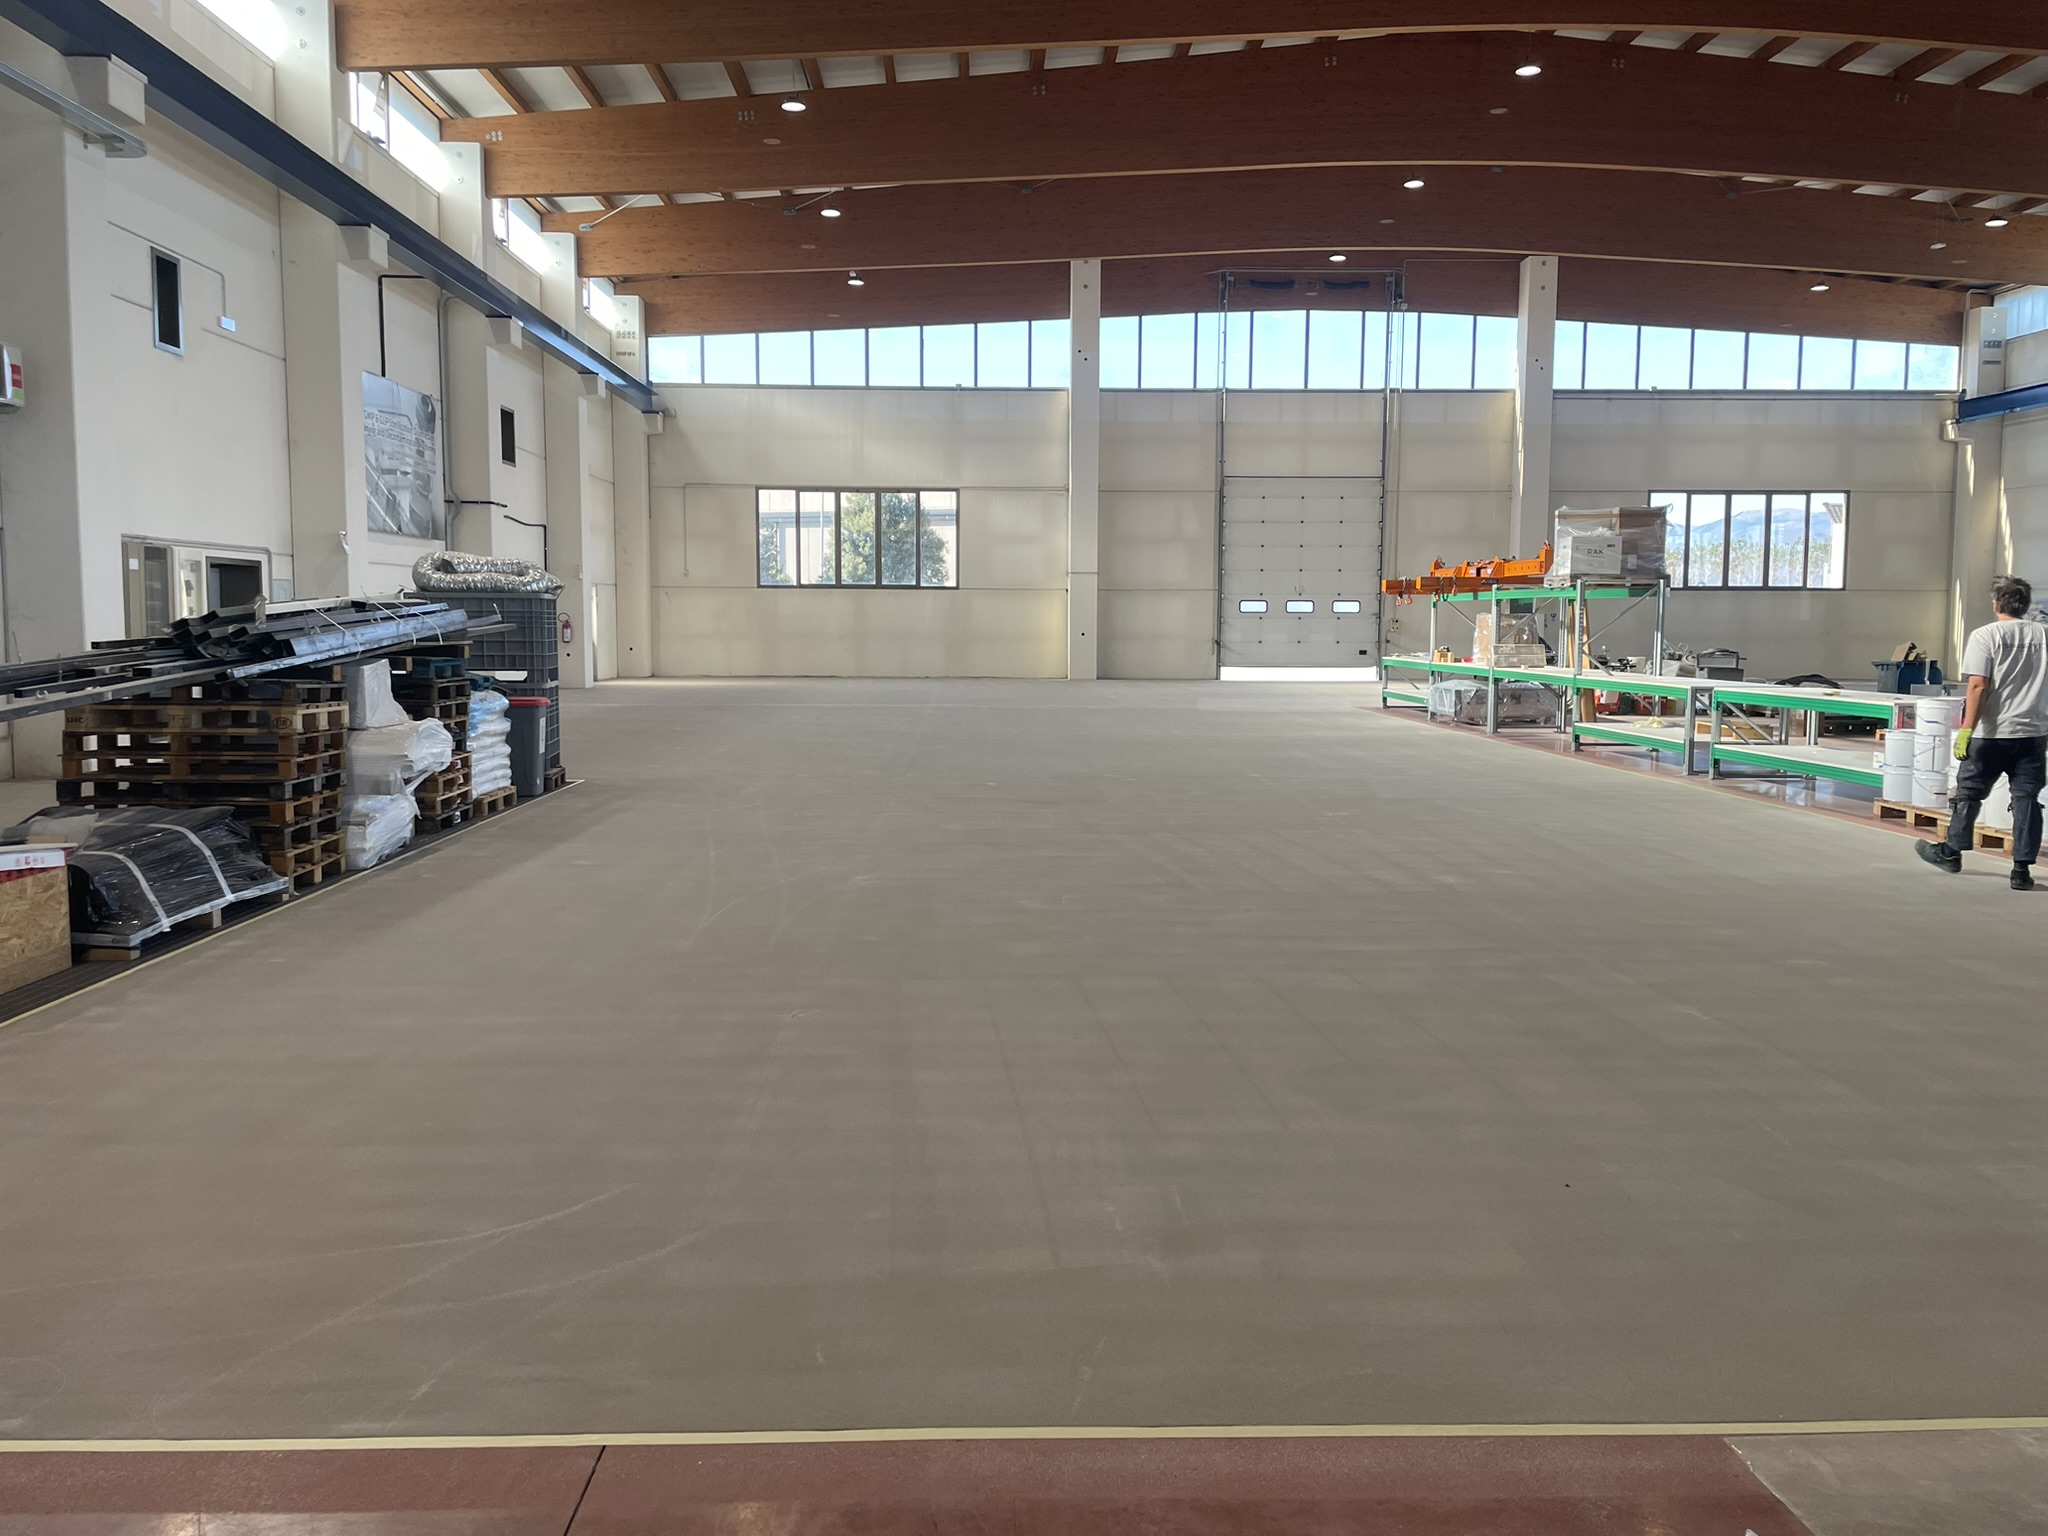
The existing substrate required consolidation, levelling, and a high-performance coating system capable of long-term durability.
Epoxy Multilayer Flooring System Application Steps
The system applied follows a structured multilayer approach, combining different technologies for maximum performance.
1. Substrate Preparation with Ecocement System
Surface preparation is always the most critical phase. The substrate was mechanically prepared to ensure:
- Adequate roughness
- Removal of contaminants
- Optimal adhesion (>1.5 MPa recommended)
The use of the Ecocement system allowed effective substrate regularisation and preparation for subsequent layers.
2. Primer Application with RESINA 530
The first functional layer was applied using RESINA 530, a low-viscosity epoxy resin with excellent penetration capacity.
Key advantages:
- Deep substrate impregnation
- High mechanical performance
- Fast curing and low odour
Applied at approx. 300–500 g/m², it ensures optimal adhesion of the entire system.
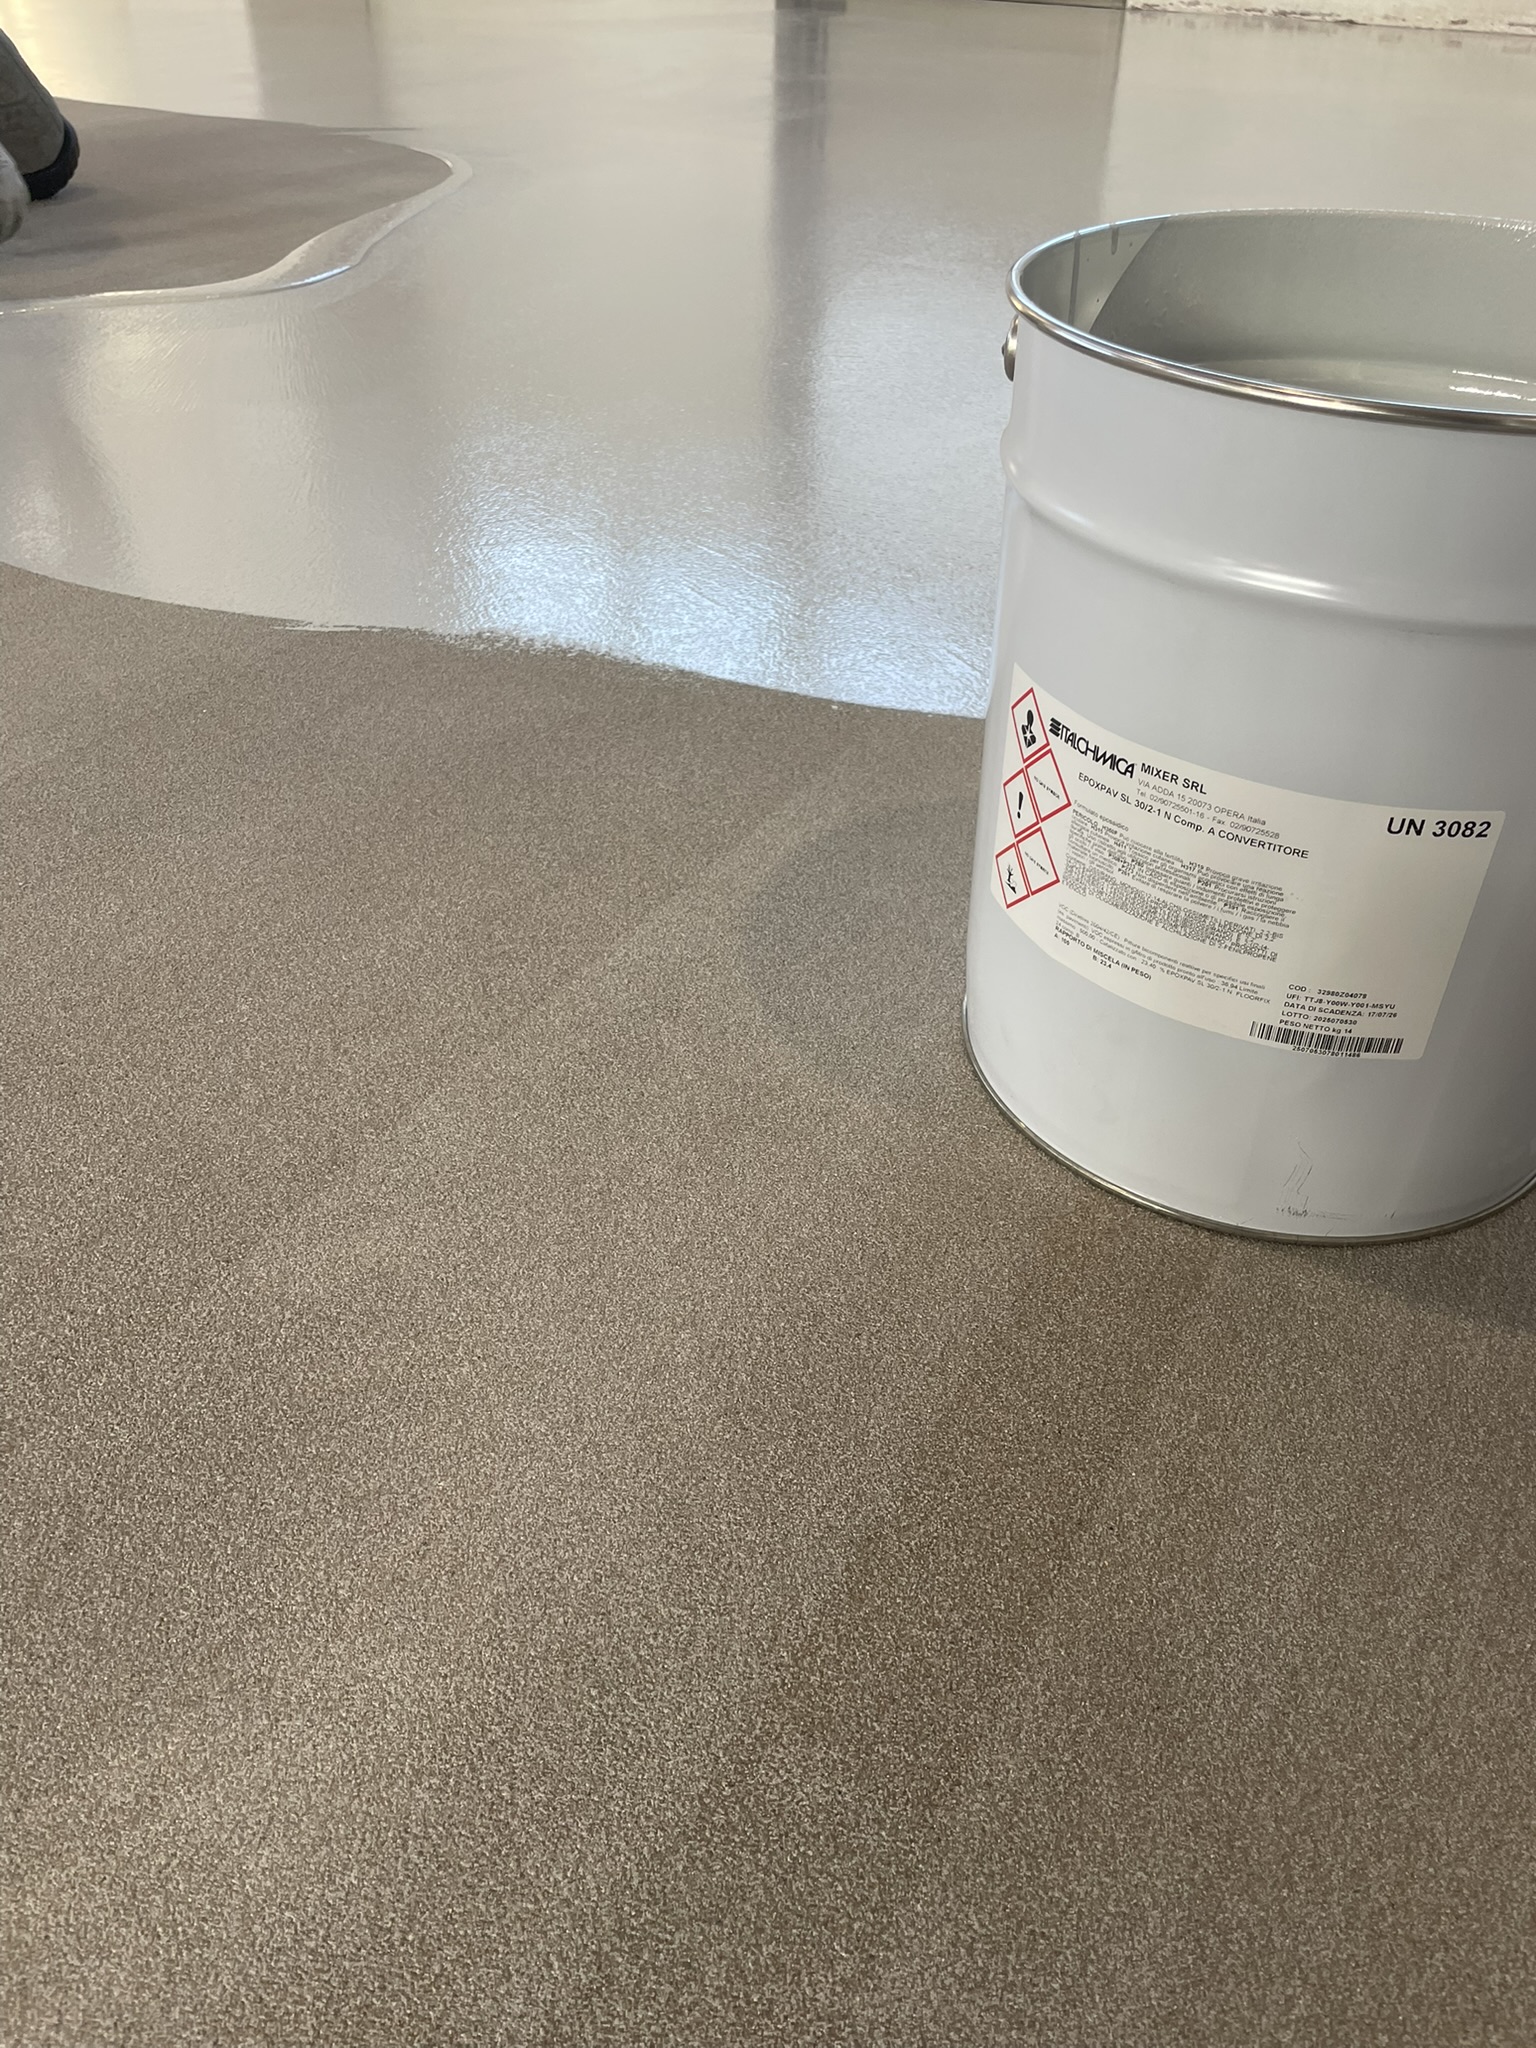
3. Multilayer Build-Up with EPOXPAV SL 30/2/1 N
The core of the epoxy multilayer flooring system is the application of EPOXPAV SL 30/2/1 N, a high-performance epoxy coating.
This layer provides:
- High resistance to abrasion and mechanical stress
- Excellent chemical resistance (acids, alkalis, oils, fuels)
- Suitable thickness from 300 µm up to 3 mm
The product was applied with quartz loading, ensuring:
- Anti-slip properties
- Increased durability
- Uniform surface texture
The repeated use of a spiked roller ensured air release and perfect levelling.
4. Polyurethane Finishing with ITALPAINT EEP
The system was completed with ITALPAINT EEP, an aliphatic polyurethane topcoat.
This finishing layer guarantees:
- UV resistance with no yellowing
- High resistance to abrasion and impacts
- Resistance to water, oils, fuels, and detergents
- Available in gloss, satin, or matte finishes
Additionally, it enhances cleanability and long-term aesthetic stability—critical in industrial environments.
Final Result: Performance Meets Aesthetics
The completed flooring system, as shown in the images:
- Offers a seamless and dust-free surface
- Improves light reflection, enhancing workspace visibility
- Integrates high-visibility safety lines for traffic management
- Ensures long-term durability under heavy use
This epoxy multilayer flooring system is ideal for warehouses, production plants, and logistics areas.
- High adhesion (>3 MPa) for long-term reliability
- Excellent mechanical strength and abrasion resistance
- Chemical resistance for industrial environments
- Fast curing times for reduced downtime
- Versatility for different thicknesses and finishes
What is an epoxy multilayer flooring system?
Where is it typically used?
Why use a polyurethane topcoat?
How thick is the system?
The epoxy multilayer flooring system represents a complete, high-performance solution for industrial flooring. By combining penetrating primers, reinforced epoxy layers, and durable polyurethane finishes, it ensures maximum reliability, safety, and longevity.
For professional applicators and contractors, this system offers a proven method to deliver high-quality, long-lasting industrial floors that meet the most demanding requirements.